
“BIG combines Advanced Hydrolock Continuous Sterilization with High-Technology Laboratory Capabilities, enabling us to control not only Food Safety, but also Particle Characteristics, Emulsion Stability, Nutritional Composition and Finished-Product Consistency.”
Advanced Manufacturing Technology. Confidence in Every Can
BIG combines Advanced HYDROLOCK Continuous Rotary Sterilization with Sophisticated in-house Laboratory capabilities to support Food Safety, Formulation Development, Physical Stability, and Finished-Product Consistency.
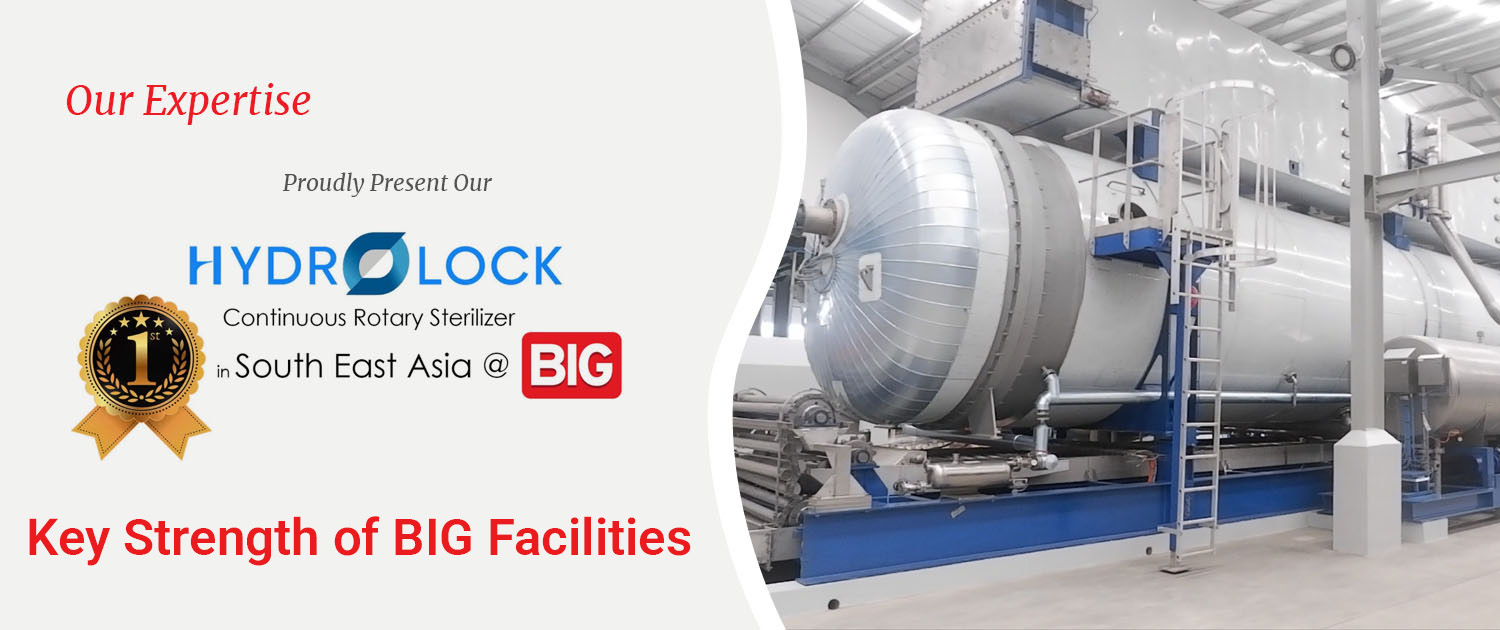
HYDROLOCK Continuous Rotary Sterilization
Our Sterilized Ready-to-Drink manufacturing capability is supported by a HYDROLOCK Continuous Rotary sterilization system enabling BIG to manufacture a broad range of shelf-stable Dairy and Beverage Products in Cans.
Consistent Thermal Processing
Controlled Temperature, Pressure, Residence time, and Rotation support a defined Thermal process. Product-specific validation and ongoing monitoring help ensure consistent achievement of the required commercial sterility targets.
Efficient Heat Transfer
Controlled CAN Rotation promotes product movement during Sterilization. For suitable products and Formulations, this agitation improves Heat Transfer within the CAN, helping achieve the required Sterilization effect efficiently.
Preserving Product Quality
With a properly validated process, efficient heat transfer can help limit unnecessary Thermal Exposure, supporting the Preservation of Flavor, Color, and overall Quality in Dairy, Coffee, and other RTD beverages.
Advanced In-House Laboratory & Quality Control
BIG’s laboratory supports Raw-Material Qualification, Formulation Development, Process Evaluation, Finished-Product Testing, and Shelf-Life monitoring
Our Analytical capabilities help translate product concepts into Consistent commercial Formulations and provide timely information for manufacturing and Quality Control Decisions.
Malvern Analytical Equipment — Particle Size & Dispersion Analysis
Our Malvern Lab equipment supports the evaluation of Particle-Size distribution and dispersion characteristics, helping our teams:
- Assess emulsions and suspended ingredients in dairy and beverage formulations.
- Optimize formulation and homogenization conditions.
- Evaluate factors affecting mouthfeel, sedimentation, and physical stability.
- Evaluate factors affecting mouthfeel, sedimentation, and physical stability.
CEM ORACLE Rapid Fat Analyzer — Fast Fat-Content Verification
Our CEM ORACLE rapid fat analyzer provides timely total-fat measurements for suitable ingredients and product samples, supporting:
- Incoming raw-material checks.
- In-process monitoring and finished-product verification.
- Consistency against approved fat-content specifications.
- Faster production and quality-control decisions.
Technology That Supports Your Brand
By combining controlled Thermal processing in HYDROLOCK with advanced Laboratory analysis.
BIG helps our Customers Develop and Manufacture Products with Consistent Quality, Reliable Performance, and Confidence for your Commercial Launch